Dimensionally Stable Anodes for Electrowinning & Electrorefining
Ir-Ta MMO and platinized titanium anodes for copper, zinc, nickel and cobalt electrowinning plus electrorefining duties. Stable cell voltage, zero lead contamination of the cathode metal, and documented coating performance — so current efficiency and energy cost stay under control.
Request a Quote Talk to an Engineer
Electrometallurgy Runs on the Anode
Copper, zinc, nickel and cobalt are recovered in tank houses where current is pushed through sulphate electrolyte between insoluble anodes and starting cathodes. For over a century the anode was lead — still true in most zinc and copper plants — and every plant pays for it in cell voltage, energy cost, anode maintenance and lead carry-over into the cathode metal.
DSA®-type mixed metal oxide (MMO) anodes change that equation. An Ir-Ta MMO anode holds a stable oxygen-evolution potential, keeps a constant inter-electrode gap because it does not deform, and releases no lead into the electrolyte — which lowers cell voltage by roughly 0.3–0.5 V in sulphate duty, cuts energy consumption per tonne of metal, and removes the lead contamination concern from cathode quality and environmental compliance at the same time.
What Limits Electrowinning & Electrorefining Performance
Four constraints dominate real tank houses — from copper SX-EW to zinc and nickel plants. Each one is addressable with the right anode and cell design.
Lead Anode Contamination
Lead-silver anodes shed lead and manganese dioxide into the electrolyte. Lead reports into the cathode metal and into the plant effluent — a metal-quality and environmental burden that tightens every year.
Cell Voltage & Energy Cost
Lead anode overpotential and the resistive PbO₂ layer on its surface push cell voltage up to 2.0–2.5 V in zinc duty. Electricity is the biggest operating cost in electrowinning — every 0.1 V saved on 1,000,000+ cells-amps means real energy and cost per tonne.
Anode Maintenance & Downtime
Lead anodes creep, buckle and build oxide scale that must be cleaned and replaced on schedule. Each stripping, straightening or replacement cycle stops the cell line and adds labour, anode stock and handling cost.
Aggressive Sulphate Electrolyte
CuSO₄/H₂SO₄ and ZnSO₄/H₂SO₄ electrolytes are hot, acidic and hard on any surface. Without a corrosion-resistant, dimensionally stable anode, the gap changes, current distribution drifts, and current efficiency and cathode quality both degrade.
Choose the Right Anode for Your Tank House
Match your electrolyte and metal duty to the correct coating and format. The table below is the fast path — our engineers refine it with your cell voltage, temperature, current density and cathode quality targets.
| Application | Recommended Anode | Coating | Current Density | Typical Life | Key Benefit |
|---|---|---|---|---|---|
| Zinc electrowinning (ZnSO₄ electrolyte) | Ir-Ta MMO plate / mesh | IrO₂/Ta₂O₅ | 0.3–0.6 kA/m² | 3–8 yrs | Lower cell voltage, no lead in electrolyte |
| Copper electrowinning (SX-EW, CuSO₄) | Ir-Ta MMO plate | IrO₂/Ta₂O₅ | 0.2–0.5 kA/m² | 3–8 yrs | Stable gap, clean cathode, less energy |
| Copper electrorefining | MMO plate / platinized Ti starter | Ir-Ta / Pt | 0.2–0.35 kA/m² | 5–10 yrs | Dimensional stability, uniform current |
| Nickel electrowinning (NiSO₄/NiCl₂) | Ir-Ta MMO plate / mesh | IrO₂/Ta₂O₅ | 0.2–0.5 kA/m² | 3–8 yrs | Chloride-tolerant coating, low overpotential |
| Cobalt electrowinning (CoSO₄) | Ir-Ta MMO plate | IrO₂/Ta₂O₅ | 0.2–0.5 kA/m² | 3–8 yrs | No lead carry-over into cathode cobalt |
| Electrolytic manganese (MnSO₄) | Ir-Ta MMO plate | IrO₂/Ta₂O₅ | 0.3–0.6 kA/m² | 3–8 yrs | Stable voltage in high-acid sulphate duty |
Ehisen Electrometallurgical Electrode Range
Six core titanium electrode formats for zinc, copper, nickel, cobalt and manganese tank houses — each coated and rated to its sulphate electrolyte with traceable material and coating documentation.
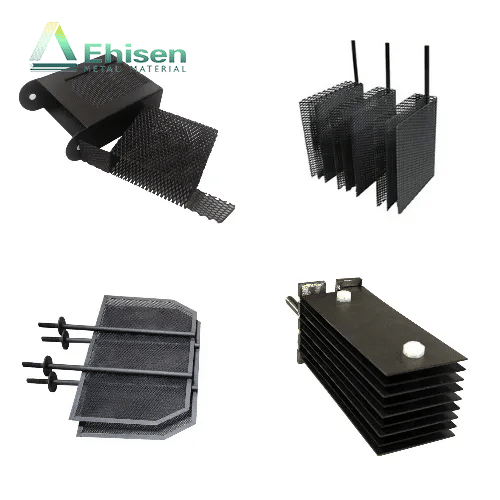
Ir-Ta MMO Plate Anode
High-stability iridium-tantalum anodes for zinc and copper sulphate duty, rated for stable cell voltage and low overpotential in hot acidic electrolyte.
| Substrate | Gr1 Ti plate / mesh |
| Coating | IrO₂/Ta₂O₅ |
| Current density | 0.2–0.6 kA/m² |
| Design life | 3–8 years at rating |

Titanium Tube & Rod Anodes
Round and tubular Ti anodes for electrorefining circuits and cells where uniform radial current distribution matters.
| Diameter | Φ16 – Φ60 mm |
| Coating | Ir-Ta / Ru-Ir / Pt |
| Current density | 0.2–1 kA/m² |
| Design life | 3–10 years |
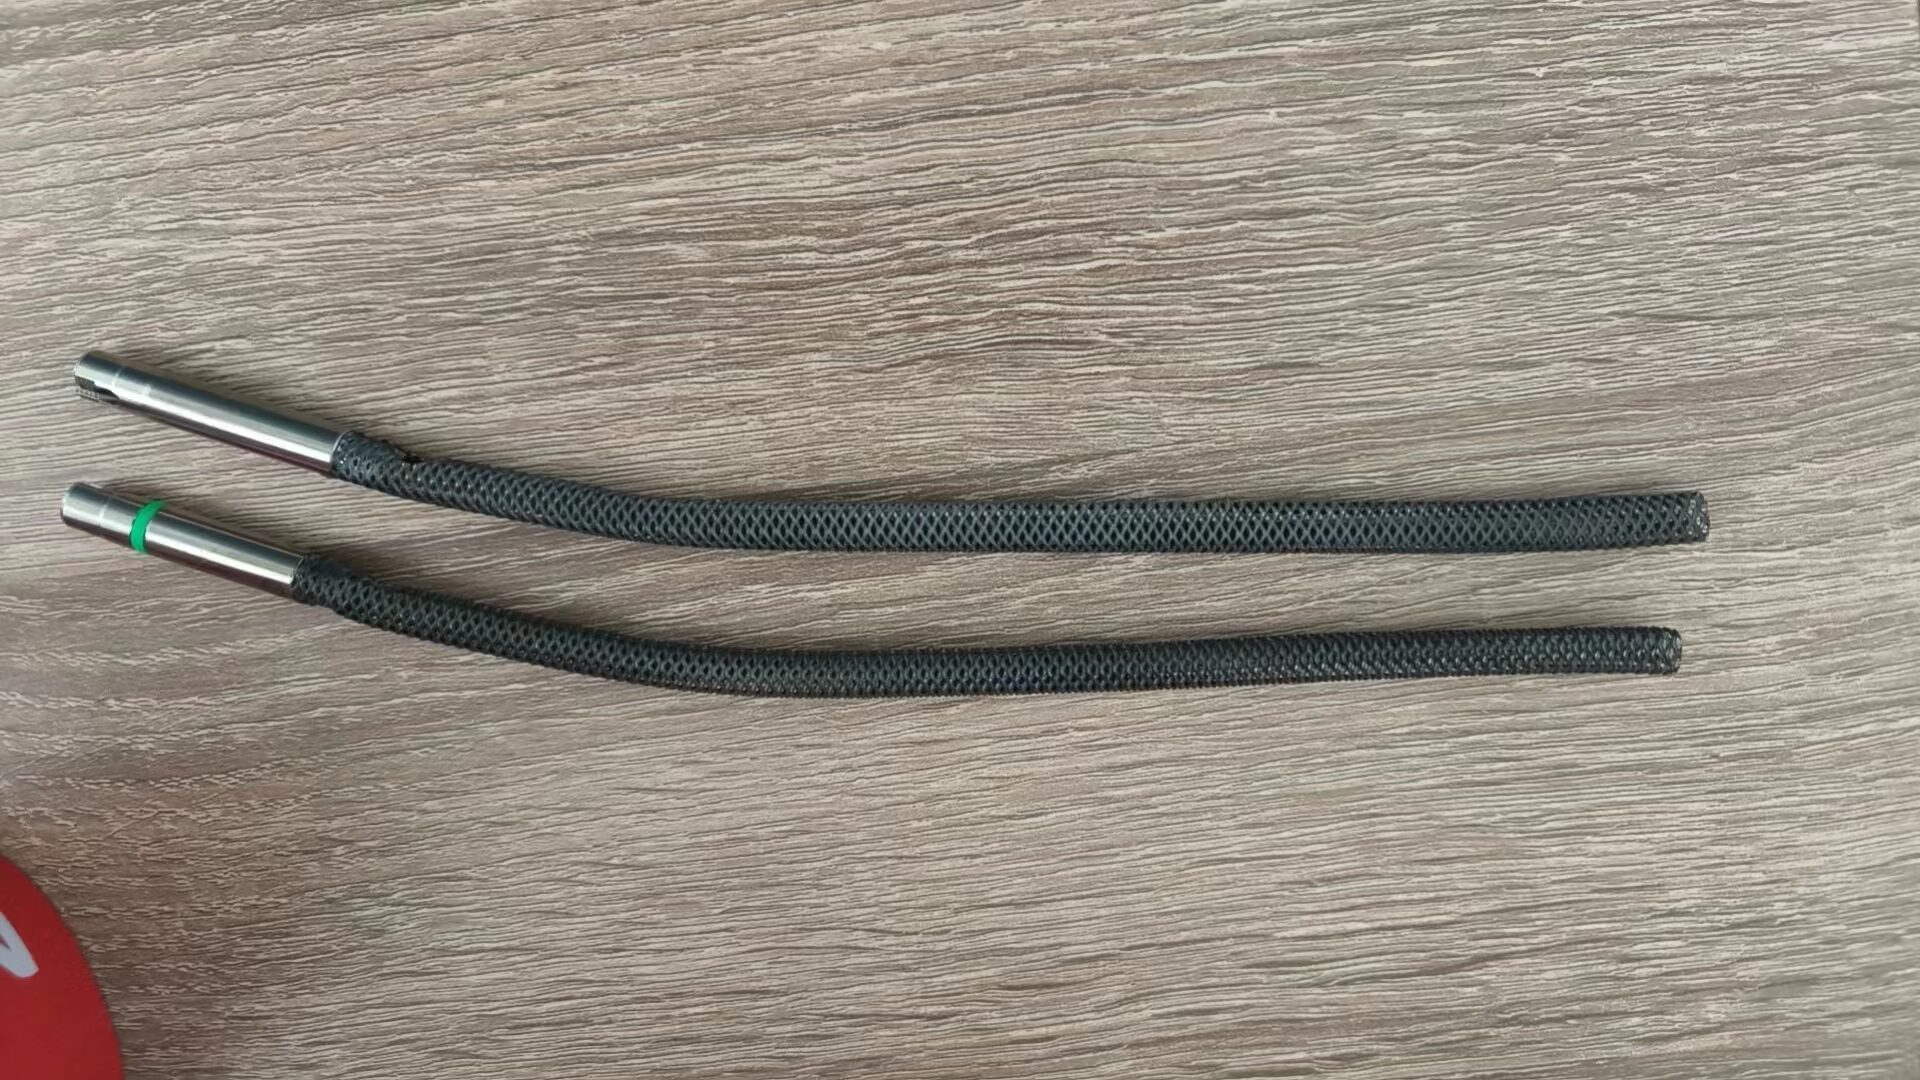
MMO Cable & Platinized Rod Anodes
Flexible MMO and platinized titanium anodes for small cells, side reactions and current-carrying auxiliary electrodes in metal winning circuits.
| Format | Cable · rod · wire |
| Coating | Ir-Ta / Pt |
| Current density | 0.2–2 kA/m² |
| Design life | 3–10 years |
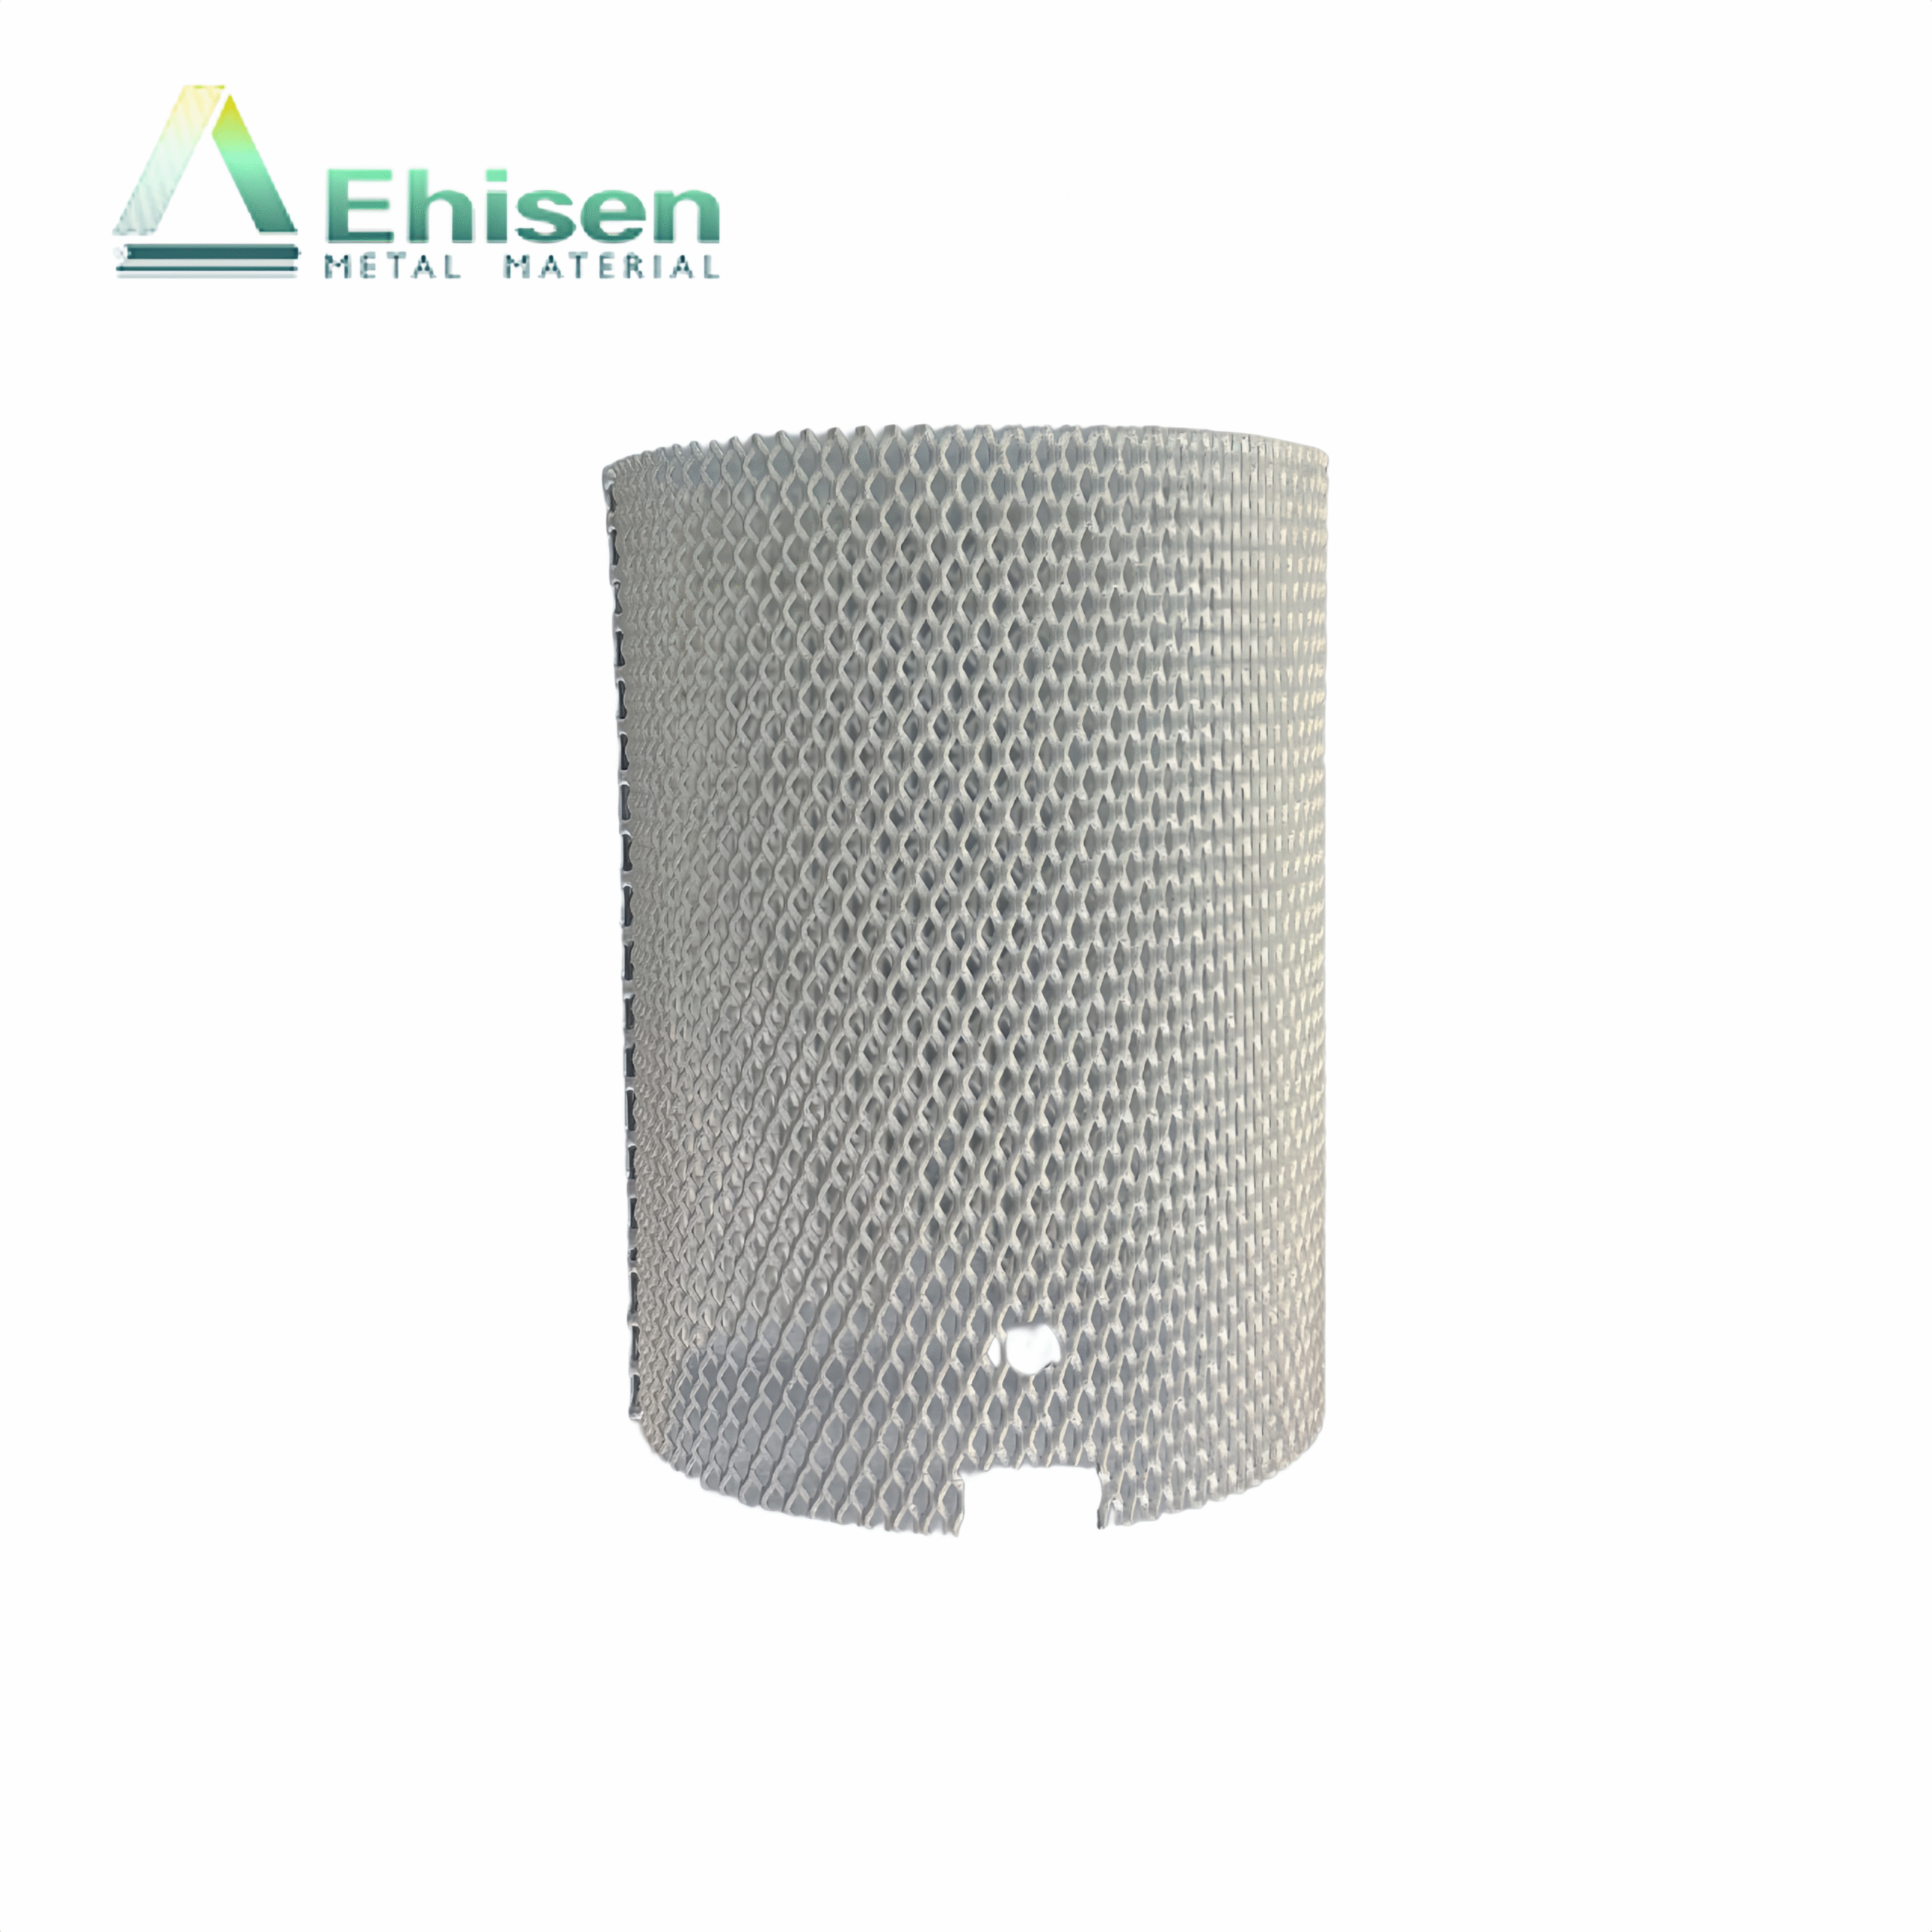
Platinized Titanium Mesh Tube Anode
Single mesh-tube electrodes with high effective surface area for nickel and copper circuits requiring low anode potential.
| Substrate | Gr1 / Gr2 Ti mesh tube |
| Coating | Pt, 5–20 g/m² |
| Current density | 0.2–1 kA/m² |
| Design life | 5–10 years |
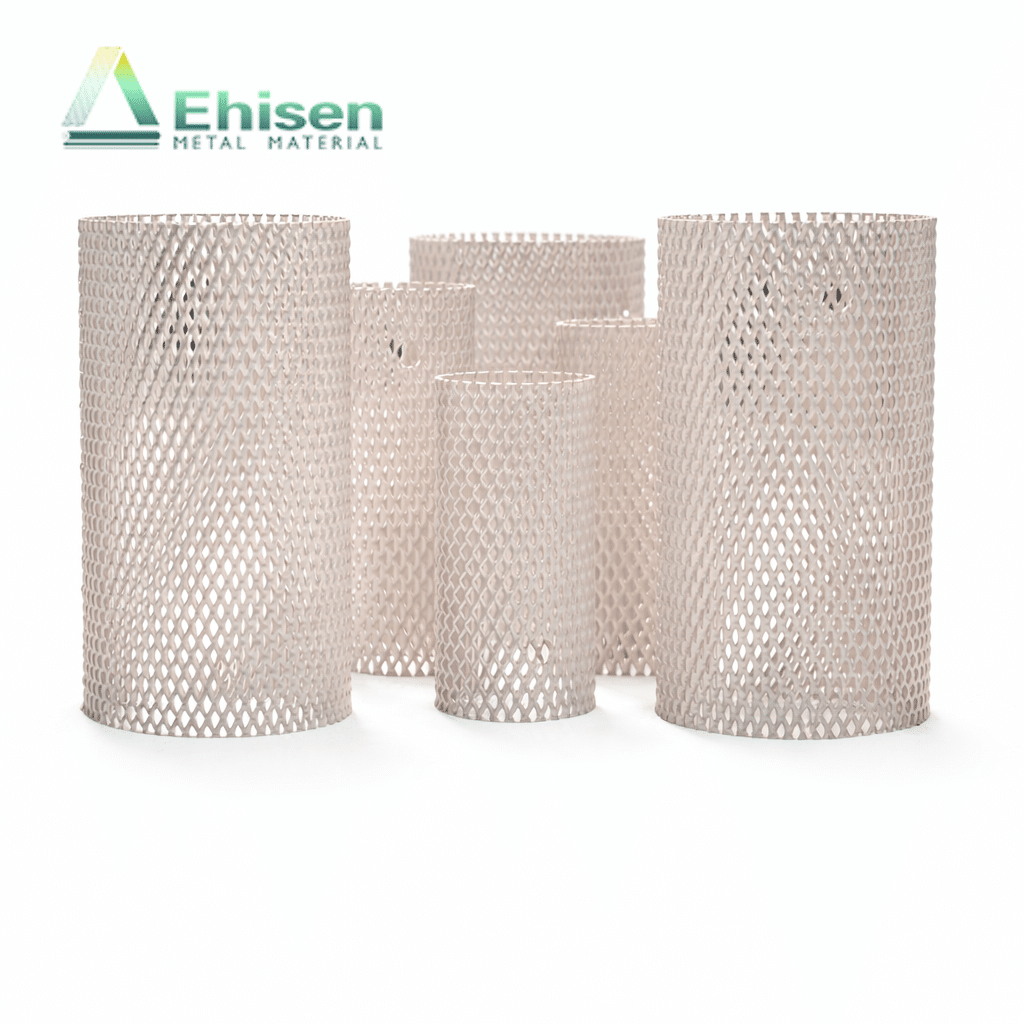
Mesh Tube Anode Cluster
Six-tube mesh clusters that spread current uniformly across the cathode face — the practical way to scale up winning cells without hot spots.
| Configuration | 2×3 / 1×6 cluster |
| Coating | Pt / Ir-Ta |
| Cell coverage | Up to 1.5 m² per cluster |
| Design life | 5–10 years |

Titanium Mesh, Blanks & Hardware
Pure titanium mesh, cathode blanks and current-distribution hardware machined and welded to your tank house geometry.
| Material | Gr1 / Gr2 Ti |
| Mesh type | Expanded · woven · welded |
| Finish | Passivated / coated on request |
| Design life | 10+ years structural |
Standard Dimensions & Output Data
Factory reference tables for the core electrowinning and electrorefining anode formats. Other sizes and precious-metal loadings can be customised on request.
| Ir-Ta MMO Plate Anode (Sulphate EW) | Size (mm) | Active Area (m²) | Current @ 0.4 kA/m² (A) | Ir Loading (g/m²) | Life (yrs) |
|---|---|---|---|---|---|
| Plate 300 × 500 | 300 × 500 × 2 | 0.30 | 120 | 10–30 | 3–8 |
| Plate 600 × 1200 | 600 × 1200 × 2 | 1.44 | 576 | 10–30 | 3–8 |
| Mesh 300 × 500 | 300 × 500 × 1.5 | 0.30 | 120 | 10–30 | 3–8 |
| Mesh 600 × 1200 | 600 × 1200 × 1.5 | 1.44 | 576 | 10–30 | 3–8 |
| Platinized Titanium Anode (Starter / Side Duty) | Pt Loading (g/m²) | Current Density (kA/m²) | Life (yrs) | Application |
|---|---|---|---|---|
| Mesh / tube / rod | 5–20 | 0.2–2.0 | 5–10 | Refining starter cells · auxiliary anodes |
| Titanium Tube Anode | Diameter (mm) | Active Length (m) | Coating | Application |
|---|---|---|---|---|
| Tube 16 mm | 16 ± 0.5 | 0.5–2.0 | Ir-Ta / Pt | Refining & high-current cells |
| Tube 32 mm | 32 ± 0.5 | 0.5–2.5 | Ir-Ta / Pt | Nickel / copper circuits |
| Tube 60 mm | 60 ± 0.8 | 0.5–3.0 | Pt / Ir-Ta | High-current cell banks |
Documented Quality for Tank House Anodes
Every anode ships with traceable substrate, coating and testing records aligned to ISO-style quality management — so plant metallurgists can trust the cell voltage, the lifetime and the audit trail.
Quality Management
All production runs under a certified quality management system with full batch traceability from titanium substrate to final test.
Material Certificates
Titanium substrate to ASTM B265 Gr1 / Gr2 with chemical and mechanical traceability.
Coating Verification
Coating thickness and iridium / platinum loading verified per batch — the parameters that actually control cell voltage, electrode lifetime and energy cost in sulphate duty.
Accelerated Life Test
Performance verified per NACE TM0108-2008 at elevated current density in the sulphate electrolyte under rated conditions.
Independent Testing
Third-party reports available on request for coating thickness, adhesion and precious-metal loading.
Project Documentation
Certificate of conformity, packing list and inspection records prepared for project handover and audits.
ALT Conditions per NACE TM0108-2008
Lifetime is verified by accelerated life testing — not field wait. We test at elevated current density in the sulphate media your tank house actually runs, then convert the data to your operating rating.
| Coating System | Medium | Current Density (A/m²) | Temperature (°C) |
|---|---|---|---|
| Ir-Ta MMO | ZnSO₄ / H₂SO₄ (zinc EW) | 20,000 | 40 ± 5 |
| Ir-Ta MMO | CuSO₄ / H₂SO₄ (copper EW) | 20,000 | 40 ± 5 |
| Pt | 10% H₂SO₄ + Cl⁻ | 40,000 | 25 ± 5 |
Specs That Keep Tank Houses Producing
Rated Current Density
Sustains efficient oxygen evolution in zinc, copper, nickel and cobalt sulphate duty without accelerated coating wear or voltage drift.
Cell Voltage Saving
Lower anode overpotential versus lead anodes — the saving that cuts kWh per tonne and total plant energy cost.
Coating Loading Tolerance
Controlled precious-metal loading per batch keeps overpotential, efficiency and lifetime consistent across the whole cell line.
Iridium Loading
Ir loading verified per batch — the loading level is what actually controls anode lifetime and the iridium cost inside your tank house.
Frequently Asked Questions About Tank House Anodes
Why replace lead anodes with MMO anodes in electrowinning?
What is the difference between lead anodes and MMO titanium anodes?
How much cell voltage can MMO anodes save in zinc electrowinning?
Will MMO anodes contaminate my cathode copper or zinc?
How long do MMO anodes last at rated current density?
Can MMO anodes be used in copper SX-EW plants?
What about chloride in nickel electrowinning electrolyte?
Why does anode dimensional stability matter?
How do I ensure sample quality matches bulk production?
Do you provide accelerated life test data for tank house applications?
What is the lead time for tank house anode orders?
How do I size anodes for my electrowinning cell line?
Need the Right Anode for Your Tank House?
Send us your cell details — metal, electrolyte composition, current density, cell dimensions and target lifetime — and our engineers will recommend the correct coating, anode format and quantity within 24 hours.
Talk to an Engineer Email UsTell Us About Your Electrowinning or Refining Cell
Complete the fields below and send — your requirements will open in WhatsApp so our engineers can reply directly.
Explore More Industry Solutions
The Components of an Electrowinning Cell House
Reliable metal production is a system result — cell, electrodes, electrolyte circulation, power supply, cathode handling and gas management must work together. Ehisen supplies the coated electrodes at the heart of the current path.
Electrolytic Cell & Busbar
The repeating cell unit where DC current deposits metal on the cathode. Cell geometry, electrode spacing and busbar sizing control current efficiency and energy use.
Anodes & Cathode Blanks
The current-discharging elements — Ir-Ta MMO or platinized titanium anodes in plate, mesh or tube format, paired with titanium or stainless cathode blanks rated to the electrolyte.
Electrolyte Circulation
Sulphate electrolyte is pumped, filtered and heated at controlled flow and temperature. Feed purity and temperature directly control coating life and deposit quality.
Rectifier & Power Feed
Rectifiers convert AC to stable, low-ripple DC cell current. Clean current keeps electrodes efficient and extends coating life.
Cathode Stripping & Handling
Deposited metal is stripped, washed and weighed on schedule. Consistent stripping cycles protect the cathode blanks and the anode gap setting.
Gas Collection & Ventilation
Oxygen (and trace acid mist) is captured above the cells and scrubbed. Good ventilation protects both personnel and the electrical busbar system.
From Cell Requirements to Installed Anodes
Building or retrofitting a tank house follows a proven four-stage sequence. Ehisen supports you at every stage with engineering input and documented hardware.
Cell Line Analysis
Electrolyte composition, temperature, cell current, current density, duty profile and target cathode quality are reviewed, then anode format, coating and precious-metal loading are calculated.
Engineering & Sample
We recommend the coating system and can supply sample anodes for testing in your actual electrolyte before full production.
Fabrication & QC
Anodes are manufactured with batch traceability, coating inspection and accelerated life testing, with full process records shipped alongside.
Installation & Trial Run
Anodes and blanks are positioned, contact resistance verified, and cell voltage and cathode quality checked during the trial run until performance is stable.
A Manufacturing Partner, Not Just an Anode Supplier
Tank house buyers choose Ehisen because coating consistency, traceability and engineering response decide how long an electrowinning anode really lasts — not just the catalogue price.
Controlled Coating
Coating applied on our own production line with a fixed formulation and controlled loading tolerance — samples and bulk runs are made to the same standard.
Full Traceability
Every batch carries a LOT number linking substrate material, coating process records, inspection results and shipping documents.
Life-Test Verified
Accelerated life testing per NACE TM0108-2008 at 20,000 A/m² in sulphate media converts laboratory hours into your tank house rating.
Engineering Support
Our engineers review your electrolyte, current density, temperature and cell geometry, then recommend coating, format and loading — within 24 hours.
Global Logistics
Export experience across 40+ countries with complete documentation: MTC, coating reports, XRF data, inspection records, certificate of conformity.
Reliable Delivery
Production planned against your project schedule, with order status updates from coating to packing list.
From Your Enquiry to Delivered Anodes
A clear, three-step process keeps every tank house order on specification and on schedule.
Send Requirements
Share your metal, electrolyte composition, current density and target coating loading via WhatsApp or email — or send a cell drawing and we will extract the parameters.
Engineering Review
Within 24 hours you receive a recommendation: anode coating, format, dimensions, loading and the supporting calculation basis.
Fabrication & Shipment
After approval, production runs with batch QC, then ships with the full document pack: MTC, coating report, XRF and ALT data and packing list.